 English
 Pусский
Powder Processing Challenges in Cosmetic Manufacturing and How to Address Them
Time: Sep 05, 2026
Content
A blush compact line at an OEM factory doubled its rejection rate from 4% to 23% in under two hours when the pre-blend began flooding through the filling hopper. Operators raised vibrator intensity, slowed the rotary press from 40 to 22 strokes per minute, and still saw cracked edges and chalky centers on nearly every tenth tablet. The formulation had not changed. The moisture content had risen from 0.3% to 0.8% after a humid night, and the effects spread to every downstream station.
The Five Common Powder Processing Failures in Cosmetic Lines
Cosmetic powder lines fail in five recognizable modes: ratholing, channeling, flooding, erratic flow, and caking. Each mode has a distinct mechanism, a visible first symptom, and a different cost on the line.
Ratholing is a flow condition in which powder discharges through a narrow vertical channel above the hopper outlet while the surrounding material stays locked in place. It differs from bridging, where powder arches completely across the outlet and stops all discharge.
Ratholing starves the press without fully stopping it, which makes it harder to detect than bridging. Channeling is the same family of failure: a narrow flow path opens, but the bulk of the hopper remains static until a sudden slump destabilizes the bed. Flooding follows when that slumped mass aerates and flows like a liquid, racing through the feeder and over-filling die cavities. Erratic flow alternates between free flow and no flow, and caking fuses particles into lumps that block screens, feeders, and fill shoes.
| Failure mode | Root mechanism | First symptom noticed | Typical impact |
| Ratholing | Cohesive powder locks against hopper walls | Slow drawdown on one side of the hopper | 10–25% capacity loss |
| Channeling | Narrow flow channel opens in static bed | Unstable fill weight on the press | Weight variation up to 8% |
| Flooding | Collapsed rathole aerates the powder | Powder pours out uncontrollably | Weight spikes and airborne dust |
| Erratic flow | Cohesion alternates with slip | Start-stop discharge from the hopper | Press stoppages and rejected compacts |
| Caking | Moisture and pressure fuse particles | Lumps in the pre-blend | Blocked feeds and hard spots in compacts |
Root Causes behind Erratic Powder Flow
Particle size, shape, surface chemistry, and moisture decide whether a cosmetic powder flows or fights the process. In compact formulas these factors interact, so a single change in one ingredient can cascade into multiple failure modes.
Mica flakes slide and interlock; talc is soft, platey, and easy to over-compact; titanium dioxide forms fine agglomerates that pack tightly. When a formula combines these with zinc stearate, minor shifts in particle size distribution restructure flow behavior completely. Fines below 50 micrometers increase cohesion, while a wide size distribution promotes segregation during conveying and filling.
Moisture is the strongest single destabilizer. At 0.5% water content most compact blends still flow; above 0.8%, liquid bridges form between particles and cohesion doubles. Glycols, humectants, and botanical extracts migrate during storage and raise moisture at the hopper. Electrostatic charge from pneumatic conveying and long blending makes fine particles cling to walls and to each other, reinforcing the same failures.
In compact production, the powder's flow function is not a material constant. It is a process state that changes with humidity, temperature, and time.
From Flow Failure to Compact Defects: The Press Connection
Flow failures reach the press as fill weight variation, and fill weight variation is the source of most compact defects. An erratic powder bed fills die cavities unevenly, and the press compresses whatever volume it receives.
Underfilled compacts come out thin, soft, and prone to edge chipping; overfilled compacts crack during ejection and leave residues on the punch face. Segregation adds a second layer: fines travel differently than coarse mica during pneumatic transfer, so color payoff and coverage shift visibly from one batch to the next.
23%rejection spikerecorded during a flood event on a rotary compact press
8%fill weight swingtypical on lines with erratic hopper discharge
90 minlost per shiftspent clearing lumps and re-establishing flow
2%powder lostas airborne dust in uncontrolled filling areas
Practical Countermeasures for Cosmetic Powder Processors
The fix is a system: hopper geometry, powder conditioning, humidity control, feed control, and automated pressing must be aligned. Taking one corrective action in isolation rarely survives the next formula change.
- Retrofit or design for mass flow. Steep hopper walls of 60–70 degrees, polished internal surfaces, and oversized outlets with anti-bridging agitators keep powder moving as a plug.
- Condition the powder before pressing. Add 0.1–0.5% fumed silica or magnesium stearate and slow-blend for 10–15 minutes to dissipate electrostatic charge and stabilize bulk density.
- Stabilize humidity at 30–40% RH. Place hygrometers in blending, conveying, and filling zones, and keep raw materials sealed until dosing. Verify moisture below 0.5% for most compact blends.
- Replace manual feeding with automated fill control. Loss-in-weight feeders or agitating auger feeders dampen density swings before powder reaches the press.
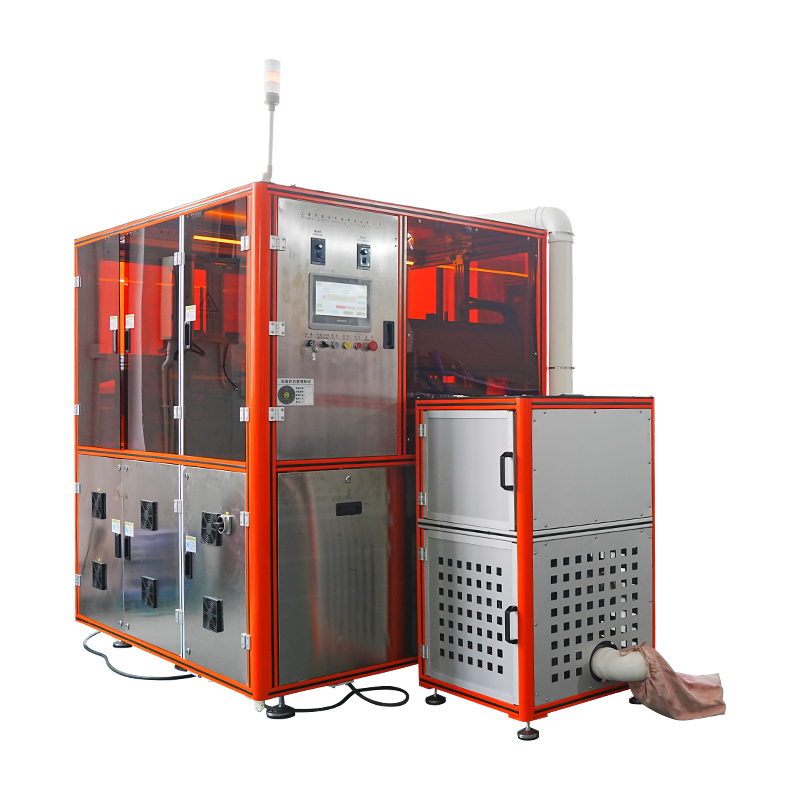
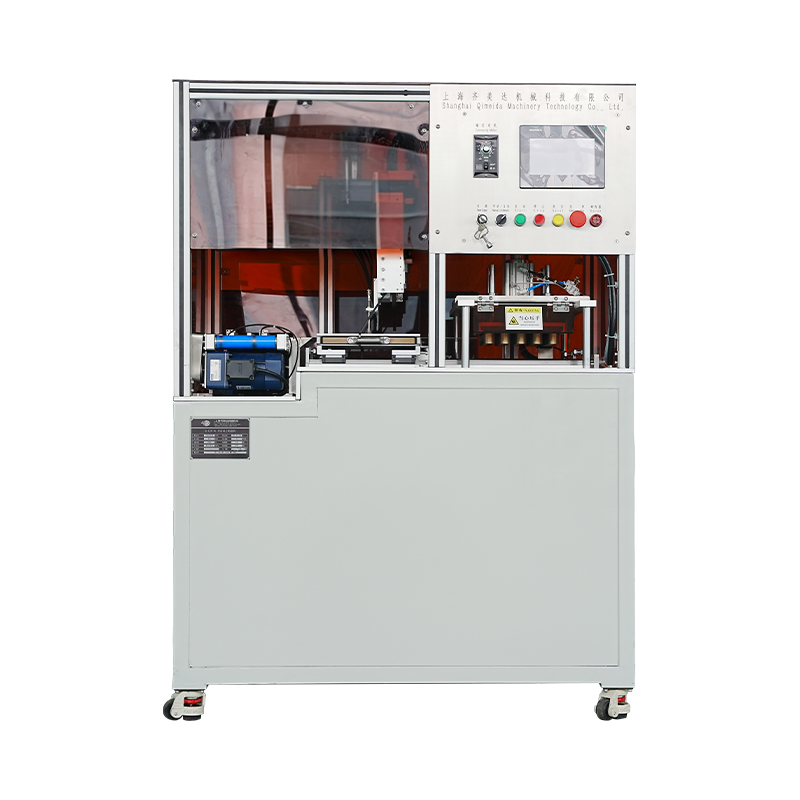
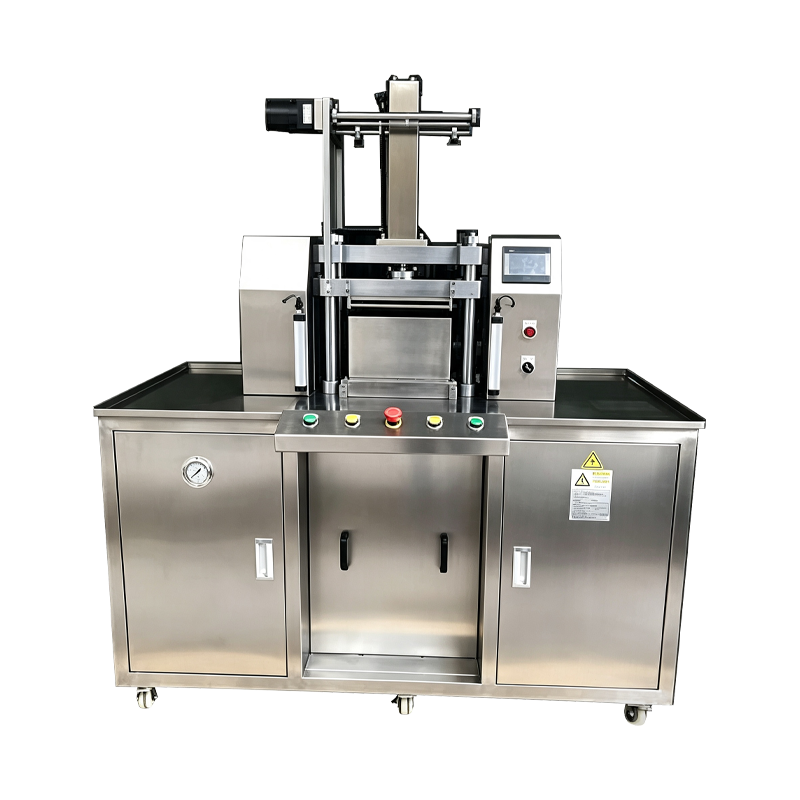
- Integrate automatic pressing with servo fill. Servo-driven fill shoes and compaction rams hold fill depth constant. For compact lines producing blush, eyeshadow, and foundation, Shanghai Qimeida Machinery Technology Co., Ltd. supplies fully automatic powder pressing solutions with automated filling, high-speed compression, and demolding stages, reducing the human variable in the pressing step.
Mass-flow hoppers are the first line of defense. If the hopper empties in first-in-first-out order and no stagnant layer forms, ratholes cannot develop and flooding is far easier to control.
Testing and Monitoring That Keeps the Line Stable
Flow testing and fill-weight monitoring catch problems before they multiply into rejects. Every new formula, every raw material lot, and every humidity swing should trigger a flow check, not a post-mortem investigation.
| Test method | What it measures | Typical good value | Typical problem value |
| Angle of repose | Loose powder pile geometry | 40 degrees or less | Above 45 degrees |
| Hausner ratio | Tapped versus bulk density | 1.25 or below | Above 1.4 |
| Carr index | Compressibility of the powder | Below 15% | Above 25% |
| Shear cell | Cohesion and flow function | Flow function above 4 | Below 2 |
| Moisture content | Water by Karl Fischer or NIR | Below 0.5% | Above 0.8% |
When a 36-cavity press starts showing a sawtooth pattern in the fill-weight trend, the powder has already begun to segregate. React to the pattern, not to the reject pile.
Frequently Asked Questions
Why does my cosmetic powder cake during storage?
Caking starts when moisture migrates from humectants, glycols, or humid air into the powder bed and forms liquid bridges between particles. The fix is to control room humidity below 40% RH, seal raw materials, and avoid stacking heavy containers on top of powder drums.
What causes flooding in a powder hopper?
Flooding happens when a rathole collapses and the falling mass aerates, turning the powder into a fluid-like suspension that races through the outlet. Mass-flow hopper geometry, agitators, and controlled discharge rates prevent the collapse-and-aerate cycle.
How do I reduce weight variation in pressed compacts?
Attack the filling stage first: use volumetric or gravimetric fill control, keep the powder level above the agitator, screen out lumps, and verify that fines are not segregating before the fill shoe. Then confirm that punch travel and dwell time are matched to the powder's response.
Can automatic pressing machines eliminate flow problems?
No machine fully compensates for a powder that will not flow, but automatic powder pressing systems with servo-controlled filling and compaction hold tighter weight tolerances and detect feed variations much earlier than manual lines. The equipment and the powder must be treated as one system.
Keep a batch record that combines flow test results, moisture readings, press speed, and compact hardness. Within two weeks, the correlation between process conditions and product quality becomes visible, and most powder processing problems become predictable.
Related products
Copyright © Shanghai Qimeida Machinery Technology Co., Ltd. All Rights Reserved.
Custom Professional Cosmetic Machinery Manufacturers
