 English
 Pусский
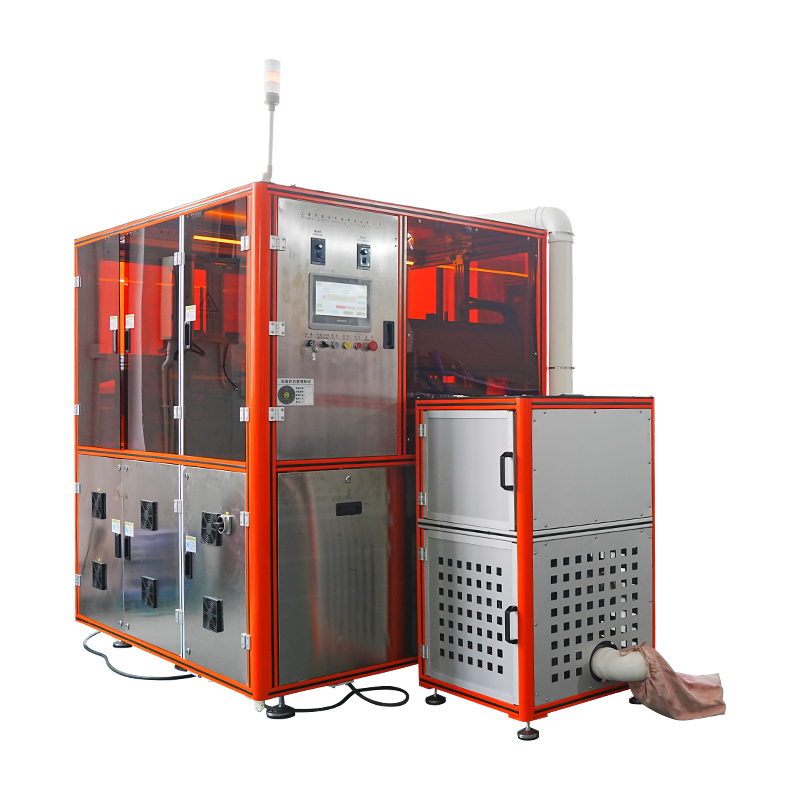
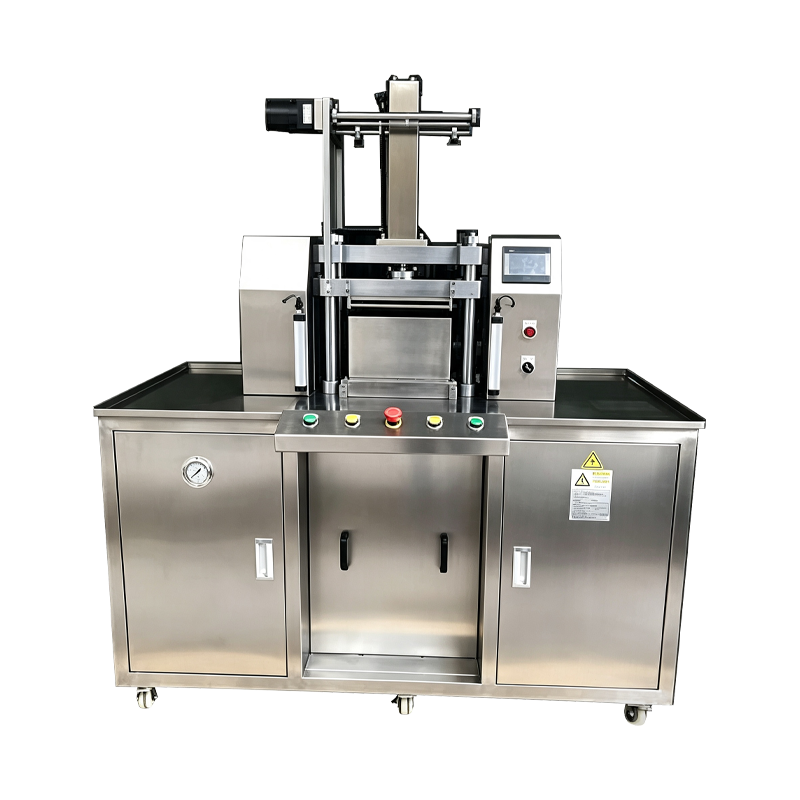
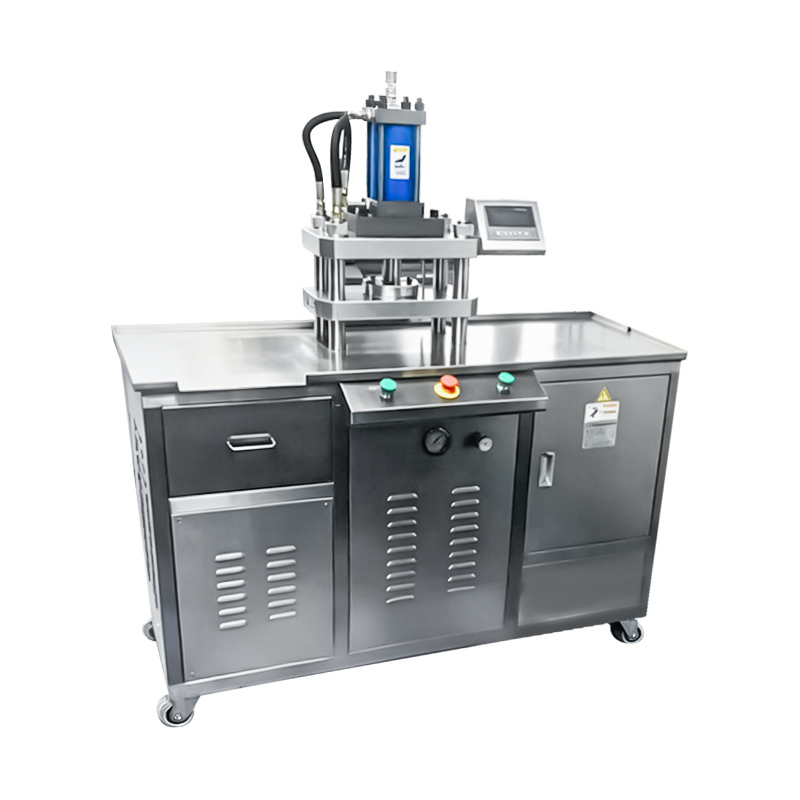
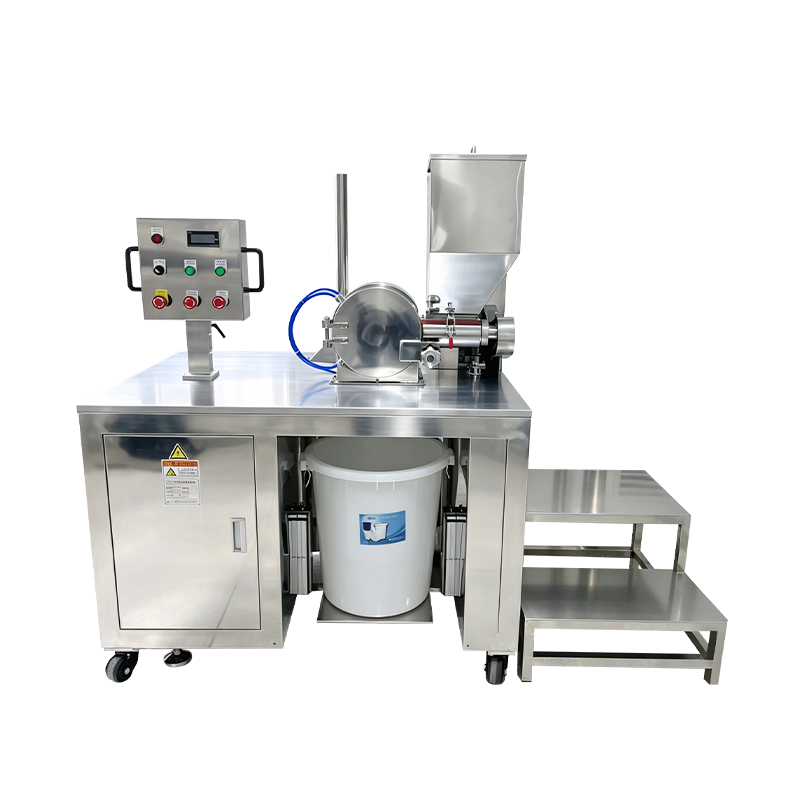
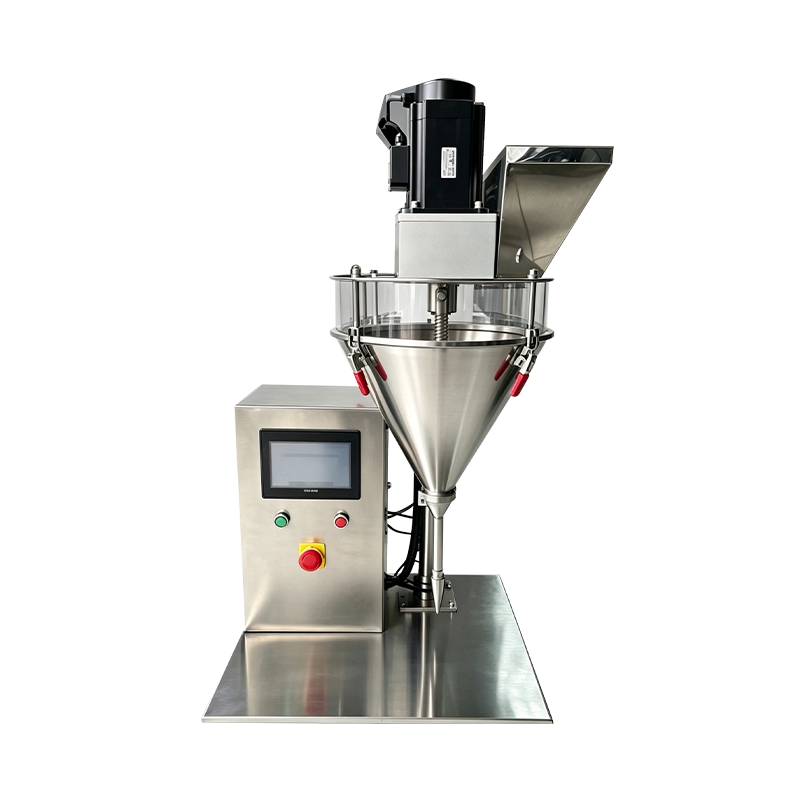
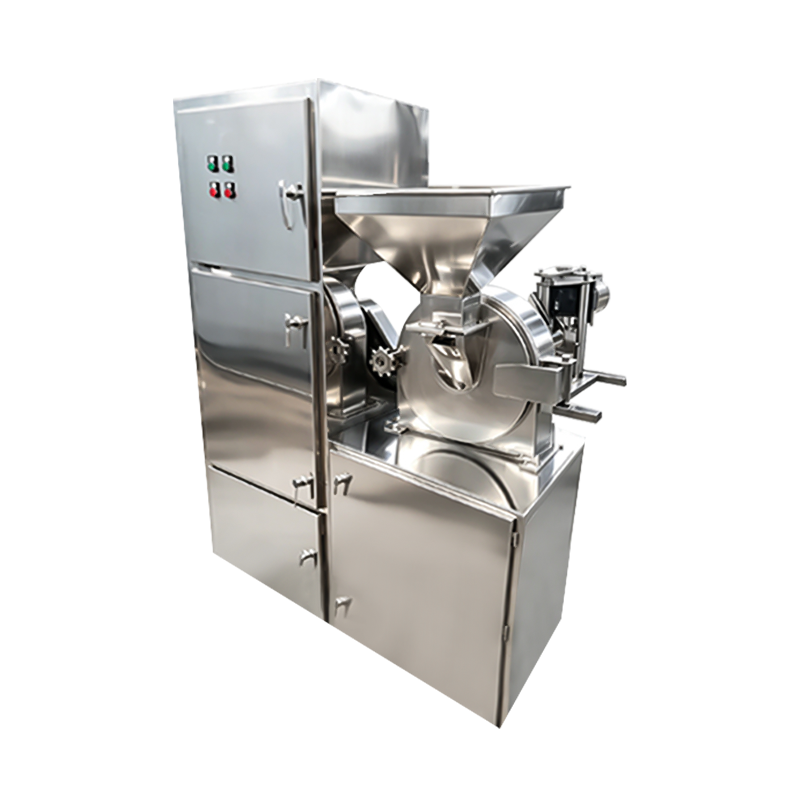
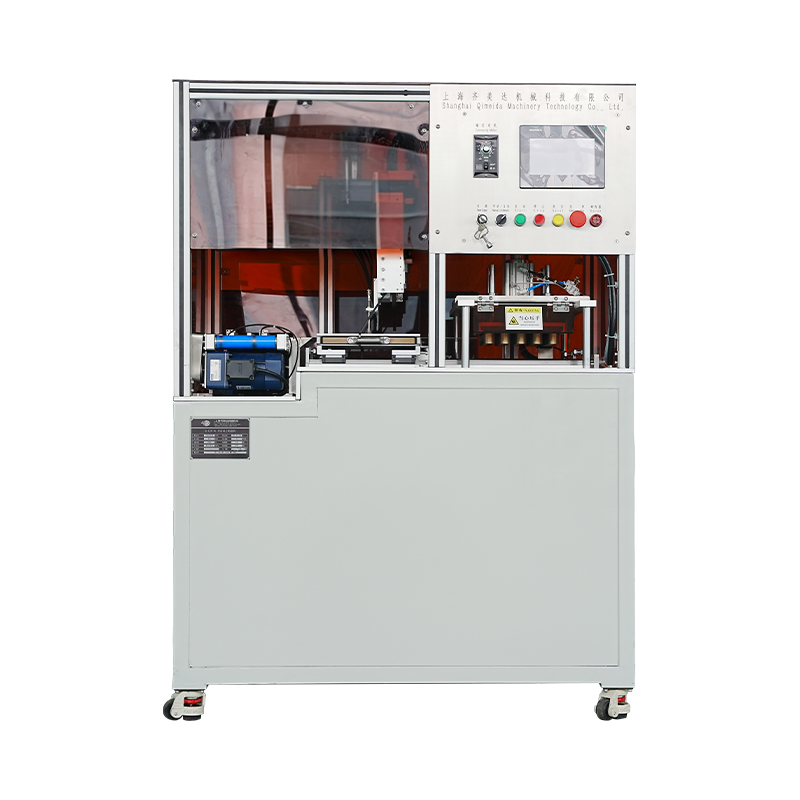
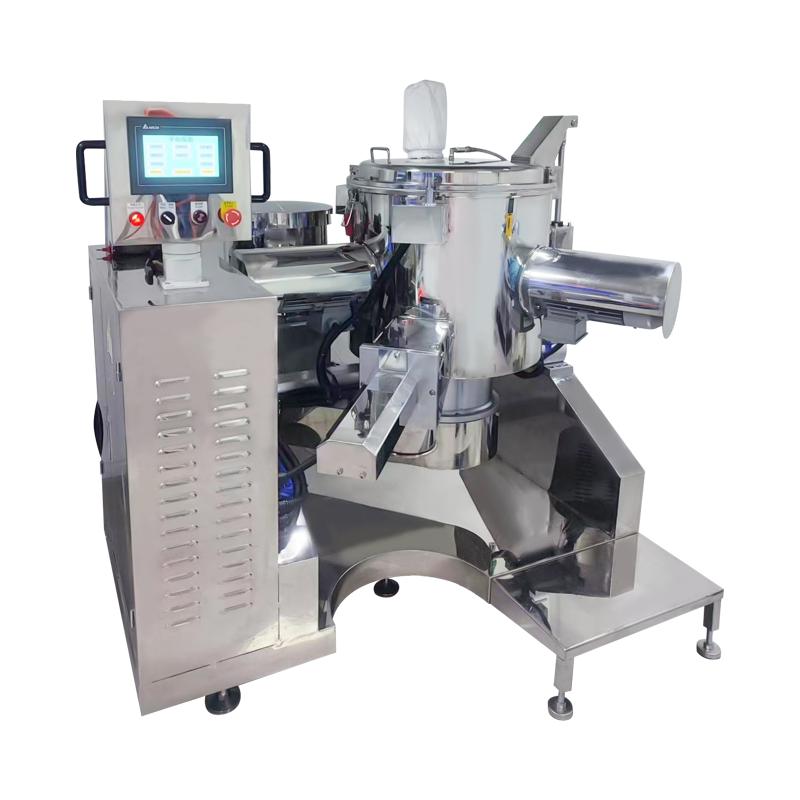
Automatic Face Powder Pressing Machine
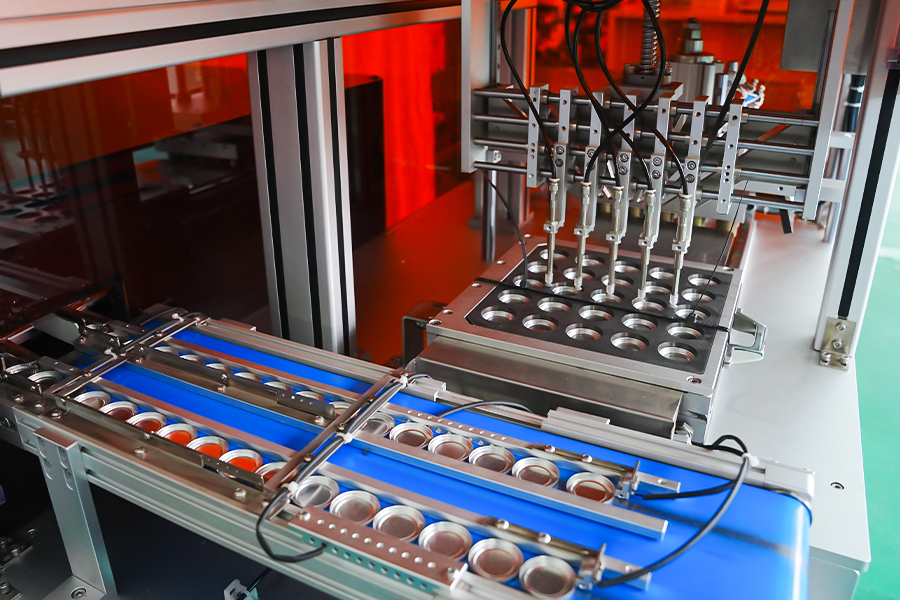
A pressing platform configured for face powder and compact powder pan production, covering large diameter flat pans, domed compacts, and pressed foundation formats. The machine automates pan feeding, powder dosing, bed leveling, compaction, and ejection in a single cycle sequence. Fill weight, pressing force, dwell time, and cycle rate are set per recipe through the HMI, and each pan cycle is logged against the batch record.
Pan Infeed
Face powder pans are presented from a tray loader or magazine into the indexing plate. Pan presence and seating depth are confirmed by sensor before the cycle proceeds.
Powder Dosing
A servo auger fills each pan to the recipe weight. An inline check weigher verifies the dose against tolerance, and out of range pans are diverted before pressing.
Bed Leveling
A scraper and light vibration step levels the powder bed inside the pan, which reduces density variation before the punch contacts the powder surface.
Compaction
The upper punch descends at a controlled rate to the set force and holds for the recipe dwell value. Force and position data are recorded for each pan.
Ejection
The pressed pan is lifted from the die and transferred to a discharge conveyor or tray loading unit. Ejection stroke is set to match pan depth.
Verification
Pan height, weight, and surface condition are checked at an inspection point. Results are linked to the batch record for traceability and deviation review.
Capabilities for Face Powder Production
Functions configured for face powder and compact powder pan formats.
Large Diameter Pans
Pan formats from 40 mm to 95 mm diameter are supported through interchangeable die plates. Larger face powder pans are available on request with adjusted force range.
Domed Compact Pressing
Domed and rounded compacts pressed with curved upper tooling. Contact velocity and compaction gradient are set per recipe to protect the dome profile.
Pressed Foundation Formats
Powder foundation pans pressed at moderate force with extended dwell to establish uniform density across the full pan diameter.
Shade Specific Recipes
Each shade and formulation stores its own fill weight, force, dwell time, and ejection setting. Recipe recall is performed from the HMI without mechanical adjustment.
Embossed Surface Pressing
Upper punches with logo or pattern relief are supported. Approach speed and compaction gradient are reduced to preserve fine detail on the pan face.
Batch Level Reporting
Fill weight, pressing force, pan count, and reject counts are logged per batch. Data exportable through OPC UA or CSV for quality review.
Technical Data
Standard configuration values. Pan size, force range, and tooling defined per project specification.
Production Fit
Where the face powder pressing machine is deployed in cosmetic manufacturing.
Volume Compact Powder Runs
Long runs of a single shade on standard pan sizes, with output stability maintained across shifts and consistent pan hardness.
Pressed Foundation Pans
Powder foundation pans pressed at moderate force with extended dwell for uniform density across the full pan diameter.
Domed Compact Formats
Domed and rounded compacts produced with curved tooling, where pressing parameters protect the dome profile and reduce edge cracking.
Seasonal Shade Transitions
Smaller batch campaigns where recipe recall and short changeover times support frequent transitions between shades and pan formats.
Embossed Compact Pans
Pans with logo or pattern relief where pressing parameters are tuned to preserve the punch detail through the compaction stroke.
Refill and Tray Formats
Refill pans and tray formats pressed with the same recipe settings, then transferred to downstream assembly for case loading.
Frequently Asked Questions
Common questions raised during evaluation and line integration. Select a question to expand the answer.
Which face powder pan formats can the machine handle
Round, oval, rectangular, and domed pan formats are supported through interchangeable die plates. Standard range covers 40 mm to 95 mm diameter or equivalent footprint, with larger formats available on request.
How is fill weight controlled for each pan
Powder is dosed by a servo driven auger using a volumetric fill method. An inline check weigher confirms weight against the recipe value, and out of tolerance pans are diverted before pressing. Fill weight is normally held within plus or minus 0.05 g.
What force range is required for pressed foundation
Pressed foundation typically uses a moderate force range with extended dwell time. The specific value depends on pan diameter, formulation binder content, and target cake hardness, and is established during factory acceptance testing.
What tooling changeover time should be expected
A full tooling set change typically takes 25 to 50 minutes, depending on pan shape and the number of positions to be updated. Tooling is stored by recipe code and staged before changeover to minimize downtime.
Can the machine press large diameter pans without density variation
Large diameter pans are supported with leveling and controlled compaction gradient stages. The bed leveling step before pressing reduces fill height variation, and the compaction gradient is set to distribute density evenly across the pan face.
What data is logged per batch
Fill weight, pressing force, dwell time, pan count, and reject counts are logged per batch. Cycle level data can be exported through OPC UA or CSV for quality documentation and process review.
What maintenance intervals apply to the press
Punch and die inspection is recommended every 500 hours, auger and dosing system cleaning at every shade change, indexer calibration every 1,000 hours, and load cell verification every 12 months. Records are kept alongside the machine maintenance log.
Can the machine integrate with existing compact case assembly lines
Yes. The discharge station provides a position identified signal that downstream case loading or tray assembly equipment can use for alignment and sequencing. Integration requirements are defined during line layout planning.
Process Deviation Reference
Situations observed during face powder pressing and the corresponding corrective actions.
Pan surface cracks after pressing
Extend dwell time by 0.5 to 1 second and reduce the compaction gradient. Verify punch and die clearance against the tooling record. Confirm powder moisture content remains between 1 and 3 percent.
Density varies across large pan diameter
Review the bed leveling step and confirm the scraper or vibration setting is correct. Extend the hold time slightly to allow the powder matrix to settle uniformly. Check the upper punch face for flatness against the tooling record.
Fill weight varies across positions
Run the per position calibration routine for the affected auger. Confirm powder bulk density consistency in the hopper and check the auger screw for wear. Verify hopper level remains above 30 percent during production.
Powder sticks to the upper punch
Reduce the pressing force by 10 to 15 percent and shorten the hold time. Polish the punch surface and confirm the release angle matches tooling specification. Verify powder temperature and moisture content before production.
Pan not fully ejected from die
Verify the ejection stroke matches the pan depth setting. Inspect the ejector rod for contamination and clean the die wall. Confirm the lower punch returns fully before the next fill stage.
Check weigher rejects exceed normal range
Verify the check weigher calibration against a reference balance. Inspect the auger and dosing barrel for powder build up. Confirm the powder supply has not shifted in particle size or moisture content between batches.
Integration Notes
Factors that affect installation, utilities, and long term operation.
Powder Supply
A buffer hopper with level feedback is recommended upstream. Powder should be dry, free of lumps, and within the specified particle size range before loading.
Downstream Transfer
The discharge station is compatible with conveyor transfer, tray loading, or robotic pick and place. A position identified signal supports downstream case loading and assembly alignment.
Tooling Storage
Punch and die sets should be stored in labeled racks with protective coating. Tooling records with clearance values accompany each pan format and recipe code.
Maintenance Planning
Recommended intervals cover punch and die inspection every 500 hours, indexer calibration every 1,000 hours, auger cleaning at each shade change, and load cell verification every 12 months.