 English
 Pусский
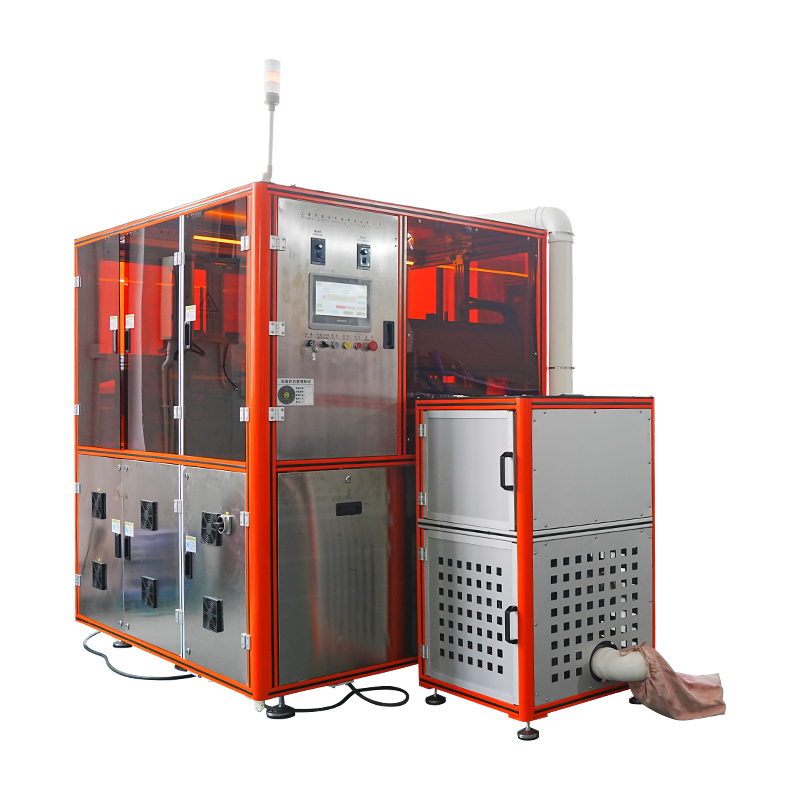
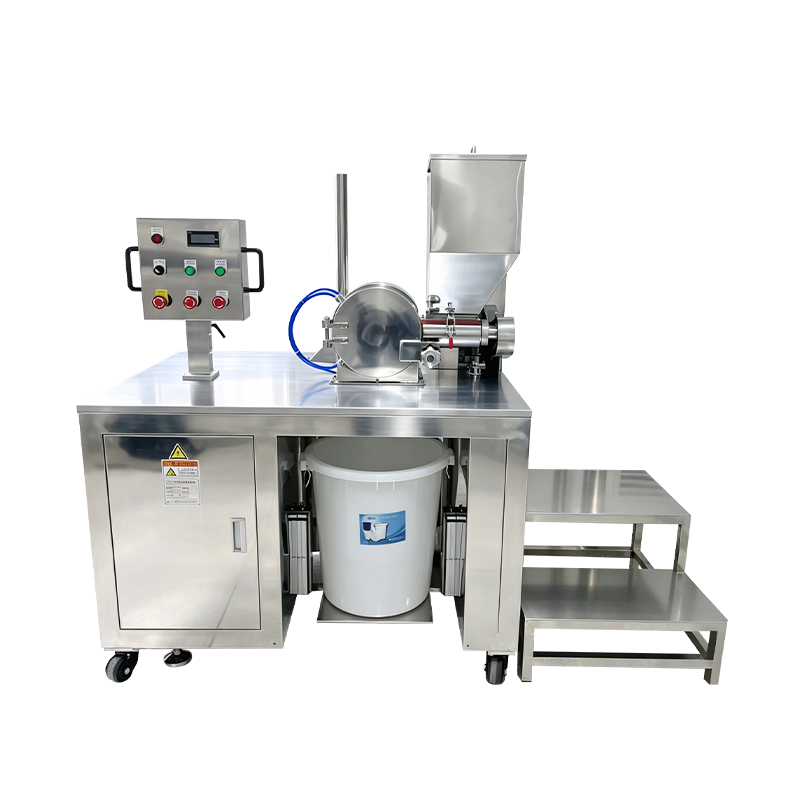
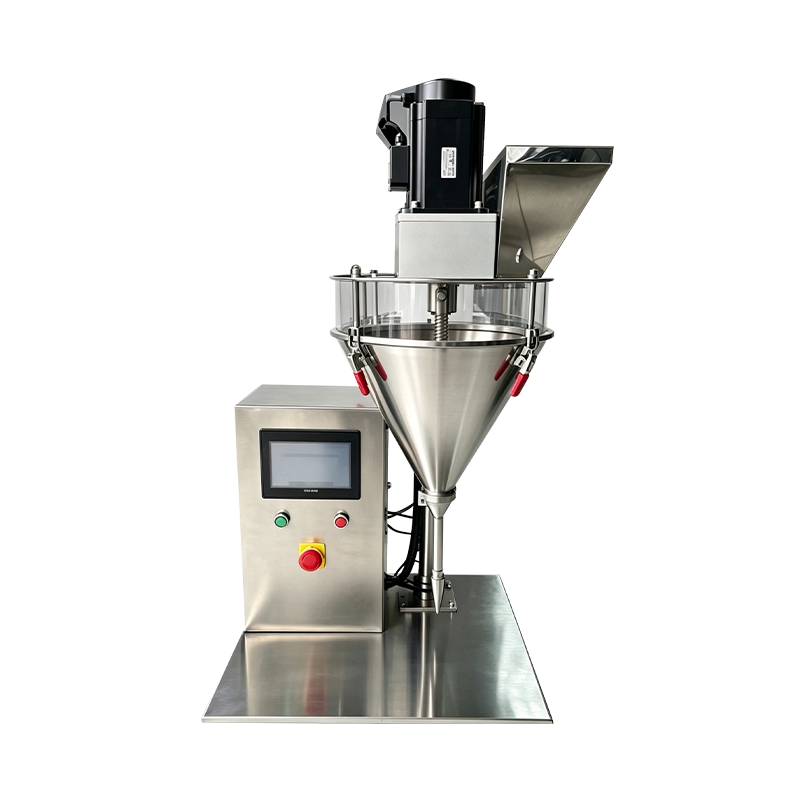
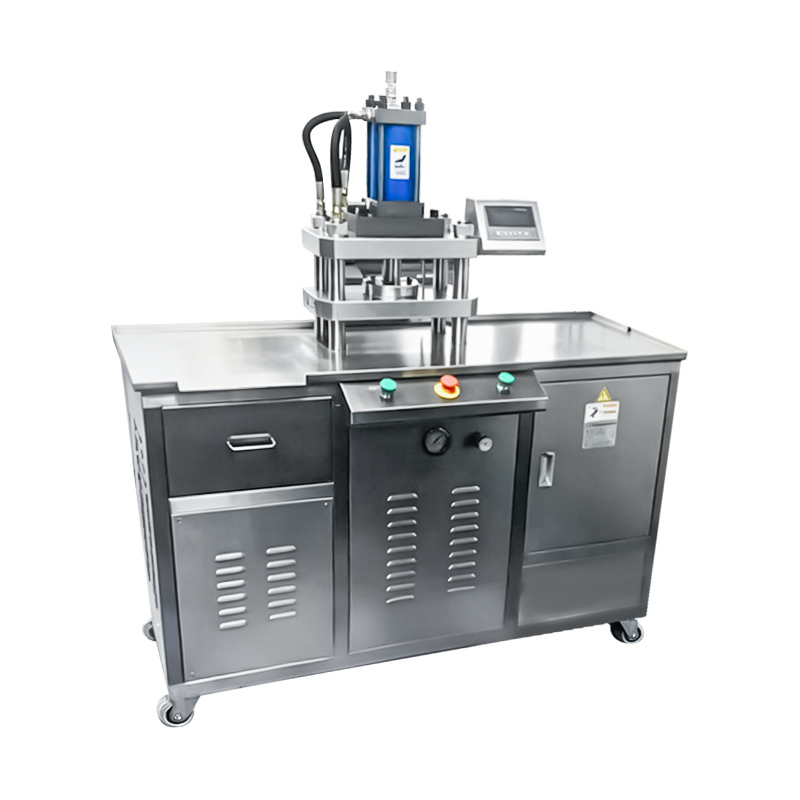
Multi Station Cosmetic Powder Press
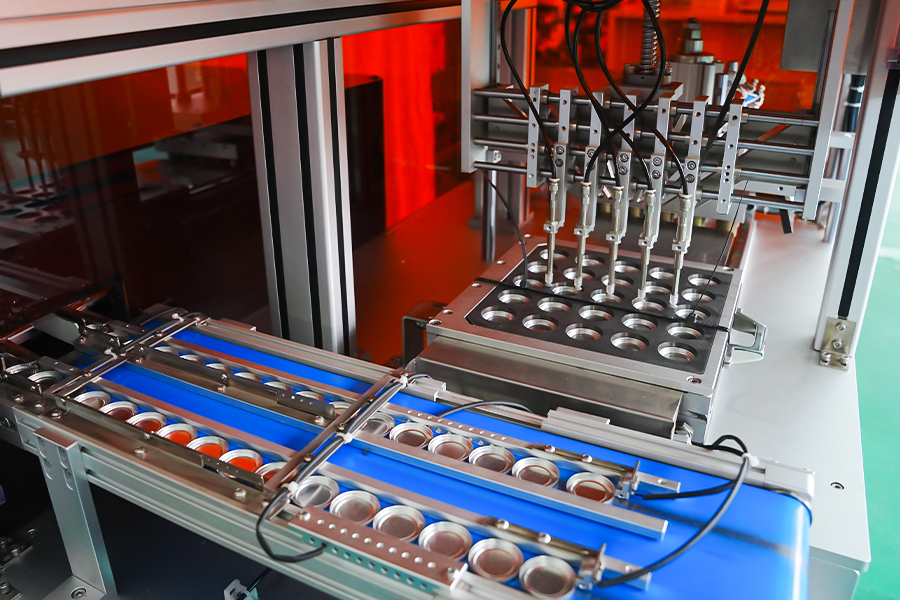
A rotary indexing platform carrying multiple pressing stations that operate in parallel, allowing simultaneous compaction of different powder formulations, pan geometries, or color variants within a single production cycle. The station count is configurable, and each station maintains independent pressure and dwell control through a centralized PLC architecture.
Production Architecture
-
Rotary Indexing Table
Servo-driven indexer positions each station with repeatability within 0.02 mm, supporting continuous cycle operation.
-
Independent Station Control
Each station carries its own pressing cylinder, pressure sensor, and dwell timer, enabling recipe variation across stations.
-
Inline Powder Dosing
Servo auger fillers synchronized with table index, filling accuracy maintained within plus or minus 0.04 g per station.
-
Centralized Data Logging
Station-level pressure, weight, and reject counts stored by batch, exportable through OPC UA or CSV.
Core Capabilities
Designed for cosmetic manufacturers running multi-SKU production on shared equipment.
Parallel Station Operation
Multiple stations press at the same time, so output scales with station count rather than cycle time. A 8-station configuration reaches 3,600 to 4,800 units per hour depending on pan size.
Mixed SKU Production
Different stations can run different formulations or pan shapes simultaneously, allowing small-batch production of multiple SKUs without line changeover.
Independent Recipe Control
Pressure, dwell time, and ejection stroke are set per station through the HMI, so one station can press a soft blush while another presses a hard highlighter.
Tooling Standardization
Punch and die sets use a common mounting interface across stations, allowing mold exchange between stations without recalibration.
Inline Reject Handling
Weight and pressure deviations trigger station-level rejection, diverting defective pans without stopping the table.
Traceability Per Unit
Each pressed pan is linked to its station, batch, and pressing parameters, supporting downstream quality documentation.
Technical Parameters
Standard configuration values. Station count and pressure range are adjusted per project specification.
Application Scenarios
Deployed in cosmetic manufacturing environments where multi-SKU flexibility and volume output are both required.
Multi-Color Palettes
Each station presses a different shade for a single palette, then the table indexes to the next shade set, reducing the need for separate lines.
Contract Manufacturing
Supports simultaneous production of multiple client SKUs in one shift, with per-station recipe recall and batch documentation.
Foundation and Compact Powder
Pressing powder foundation and compact powder pans at high volume with per-station pressure control for different shade hardness.
Pressed Pigment Manufacturing
Compacting pressed pigments and mineral powders into various pan geometries, including domed and beveled formats.
High Volume Single SKU
All stations run the same recipe for maximum throughput on a single product, reaching up to 7,200 units per hour.
Pilot and Scale-Up Production
Lower station counts used for formulation trials, then scaled to higher station counts without changing process parameters.
Operational Questions
Common production and maintenance situations encountered by line operators and process engineers.
Weight variation between stations
Recalibrate the servo auger on the affected station using the HMI calibration routine. Verify powder bulk density consistency in the hopper and confirm the auger screw is not worn. Cross-check the station pressure sensor reading against the master gauge.
Table indexing position drift
Check the servo indexer encoder coupling for backlash. Verify the table locking mechanism engages fully at each station. Run the indexer homing cycle and inspect the mechanical stop for wear. Confirm lubrication of the rotary bearing per schedule.
Uneven compaction across stations
Compare pressure curves per station through the HMI trend screen. Inspect for hydraulic pressure drop on specific stations. Verify punch and die clearance is within specification. Check that the dwell timer is correctly set for each recipe.
Reject rate increases at one station
Isolate the station by running a test batch with that station bypassed. Inspect the ejection rod for powder buildup or scoring. Verify the weighing sensor zero point and check for vibration interference from adjacent stations.
Changeover time exceeds target
Standardize tooling storage by station number and recipe. Pre-stage punch and die sets before changeover begins. Use quick-release clamps and verify that all stations use the same mounting interface. Record changeover steps in the recipe for operator reference.
Integration Notes
Considerations for line integration, process control, and long-term operation.
Upstream Feeding
The press interfaces with upstream powder blending and conveying systems through a buffer hopper. Level sensors maintain consistent feed to each station auger.
Downstream Handling
Pressed pans are transferred to a take-out conveyor or robotic arm. The press outputs a station-identified signal for downstream sorting and packaging.
MES and Batch Records
Station-level production data can be pushed to MES or ERP systems through OPC UA, supporting batch traceability and yield reporting.
Preventive Maintenance
Recommended schedule covers hydraulic oil analysis every 2,000 hours, punch and die inspection every 500 hours, and indexer calibration every 1,000 hours.